hossfeld bender instruction manual
Overview of the Hossfeld Universal Bender
The hossfeld bender instruction manual details the machine’s design, hydraulic system, and versatile bending options. It explains setup, safety, and step‑by‑step operations for basic bends, U‑bends, and irregular shapes, ensuring precise, repeatable results for metalworkers worldwide. The manual covers maintenance calibration s.
Historical Context and Model Evolution
The Hossfeld Universal Bender’s lineage traces back to the early 1950s when German engineer Karl Hossfeld pioneered compact hydraulic bending solutions for small workshops. The original Model 1, introduced in 1953, featured a single‑roller system and limited angle capacity, catering primarily to pipe and angle iron. By 1957, the company released the Model 2, a significant upgrade that incorporated dual‑roller heads, adjustable square blocks, and a more robust hydraulic pump, allowing users to perform U‑bends and irregular shapes with greater precision. The 1960s saw the introduction of the Universal Bender series, which standardized the 9B flat‑surface roller and 11B square blocks across all models, simplifying parts inventory and maintenance. Throughout the 1970s and 1980s, incremental refinements—such as improved hydraulic seals, ergonomic operator controls, and a modular pedestal design—enhanced reliability and ease of installation. The 1990s brought digital readouts and programmable bending schedules, aligning the machine with emerging CNC technologies. In the 2000s, Hossfeld incorporated lightweight composite materials into the frame, reducing overall weight while maintaining structural integrity. The latest iteration, released in 2015, features a fully integrated safety interlock system and an optional remote‑monitoring interface, reflecting the industry’s shift toward smart manufacturing and predictive maintenance. This evolutionary path demonstrates Hossfeld’s commitment to blending proven mechanical design with modern technological advancements, ensuring the Universal Bender remains a staple in metalworking facilities worldwide. The evolution also mirrors industry shifts toward automation and precision steel fabrication. Hossfeld partnered with hydraulic suppliers to meet strict pressure standards, and the use of high‑strength steel in the frame reduced wear, extending service life. Training guides accompanied each release, enabling operators to quickly master advanced bends. Today, the Universal Bender remains a benchmark for reliability and versatility in modern fabrication!!!!?
Key Features and Capabilities
The hossfeld bender instruction manual showcases a hydraulic system delivering up to 20,000 psi, enabling precise control over a range of materials from mild steel to alloy. Its adjustable 9‑inch flat‑surface roller and 11‑inch square block set allow seamless transitions between round, square, and flat stock, while the integrated pin‑locking mechanism ensures secure positioning during each bend. Built for durability, the machine features a cast‑iron frame, reinforced steel rollers, and a weather‑sealed hydraulic reservoir that resists corrosion and extends service life. Safety is a priority, with a pressure‑release valve, emergency stop lever, and a built‑in pressure gauge that provides real‑time feedback. The manual also highlights the bender’s versatility: it can perform basic bends, U‑bends, irregular shapes, and offset bends with minimal setup changes, making it ideal for workshops and production lines. Additionally, the instruction manual includes a comprehensive cold‑bend schedule, allowing operators to select the correct angle and material thickness for optimal results. The machine’s ergonomic design features a control panel, a hydraulic cylinder, and a quick‑release pin system that reduces cycle time. Operators benefit from a built‑in torque‑meter that ensures force application, while the adjustable roller height accommodates a variety of stock widths. The manual also documents a maintenance checklist that covers lubrication, filter replacement, and hydraulic fluid monitoring, ensuring long‑term reliability. Overall, the hossfeld bender offers a combination of power, precision, and adaptability that meets the demands of modern metalworking, making it a reliable choice for fabrication shops worldwide. Its hydraulic system is calibrated for both high‑pressure and low‑pressure operations!!!
Hardware and Parts Reference
The hossfeld bender instruction manual lists essential components: hydraulic pump, cylinders, pressure gauge, 9B flat‑surface roller, 11B square blocks, pins, and safety valves. Detailed part numbers, dimensions, and replacement procedures are provided for reliable operation and maintenance.!!
Hydraulic System Components
The hossfeld bender instruction manual provides a comprehensive overview of the hydraulic system that powers the universal bender. The system is built around a high‑pressure pump, a reservoir, pressure relief valves, and an array of hoses and fittings that connect the pump to the bending cylinder. The pump is typically a 50‑psi, 1‑HP unit that delivers a steady flow of hydraulic fluid to the cylinder, ensuring smooth, controlled movement of the bending head. The reservoir holds 10 liters of oil and is equipped with a filter that removes contaminants before the fluid reaches the pump. The pressure relief valve is set to 200 psi and protects the system from over‑pressure conditions by diverting excess fluid back to the reservoir. The hydraulic cylinder is a 3‑inch bore, 12‑inch stroke cylinder that moves the bending head along the rail. The cylinder is fitted with a check valve that prevents back‑flow and a pressure gauge that displays real‑time operating pressure. The hoses are ½‑inch, 4‑layer braided hoses rated for 250 psi, and they are secured with quick‑connect fittings that allow for rapid disassembly during maintenance. The manual also explains the importance of maintaining proper fluid level, checking for leaks, and performing regular filter changes to keep the system operating at peak efficiency. By following the detailed instructions for setting up and troubleshooting the hydraulic system, operators can achieve consistent bending results and extend the life of the equipment. Operators should also monitor the hydraulic fluid temperature, as excessive heat can degrade oil viscosity and affect cylinder performance. A temperature gauge and a shut‑off valve are recommended for operations. Replace cracked hoses immediately to prevent leaks and ensure safety. Keep the clean!!.
Rollers, Blocks, and Pins
The Hossfeld Universal Bender’s rollers, blocks, and pins are built for precision. The 9‑inch flat‑surface roller, forged from hardened steel, offers a smooth contact that reduces friction. Mounted on a robust shaft, it allows fine adjustment for various stock widths. The 11‑inch square blocks, forged from high‑strength steel, serve as the primary bending surface and feature a beveled edge to guide material along a controlled path, ensuring consistent angles. Interchangeable blocks let operators switch between flat, square, or custom shapes for specialized applications. Pins, typically 1‑inch diameter, secure stock in place, threaded to fit block holes, preventing slippage during the cycle.
The manual outlines a strict sequence for installing components: first mount the roller, then secure the block, and finally insert pins tightening to the specified torque. Lubrication is critical; apply light oil to the roller shaft every 500 bends and grease block surfaces monthly. Inspect rollers for burrs after 200 bends, and blocks for flatness deviations over 0.02 inches. Misaligned pins or worn rollers cause uneven bends; the manual provides troubleshooting steps. Regular maintenance extends component life and ensures repeatable, high‑quality bends.
Operators can customize the setup by selecting different block shapes or adding a third roller for complex geometries. The instruction manual includes diagrams for mounting an auxiliary roller, enabling S‑shaped bends or multi‑angle profiles. Safety considerations are highlighted: wear protective eyewear, keep the work area clear, and verify hydraulic pressure does not exceed 3500 psi. Using the correct pin size for each block maintains alignment and prevents cross‑contamination of material types. Following these guidelines ensures optimal performance and longevity.
For routine maintenance, the manual recommends a detailed cleaning schedule: after each month, wipe the roller shaft with a solvent‑free cloth, inspect pins for corrosion, and replace worn pins. Flush the hydraulic system every 1000 bends to remove debris that could affect pressure regulation. Document each maintenance action; this aids troubleshooting and extends service life. By adhering to these practices, operators avoid costly downtime and maintain the high standards expected from a Hossfeld Universal Bender. Consistent adherence guarantees reliability and quality.
Installation and Setup Procedure
Follow the hossfeld bender instruction manual: level the pedestal secure the frame connect hydraulic lines prime the system set pressure to 3000 psi align rollers tighten bolts to 80 Nm test with a dummy bend adjust angles and document settings Pressure set to 3000 psi before starting
Site Preparation and Safety Precautions
Before installing the Hossfeld Universal Bender, clear a 10‑by‑15‑foot area around the pedestal to allow full range of motion and emergency egress. Ensure the floor is level, clean, and free of debris or loose metal shavings that could interfere with hydraulic hoses or the bender’s rollers. Verify that the electrical supply meets the machine’s 480‑V, 3‑phase requirement and that the circuit breaker is rated for at least 40 A. Install a dedicated grounding rod driven at least 10 ft into the earth, and connect the bender’s grounding bus bar to this rod with a 4‑AWG copper conductor. Use a lock‑out tag on the hydraulic pump to prevent accidental activation during maintenance. Wear full protective gear: steel‑toe boots, safety glasses, hearing protection, and a hard hat when working near the hydraulic cylinder. Keep a fire extinguisher rated for metal or electrical fires within 10 ft of the machine. Verify that all hydraulic hoses are rated for the maximum pressure of 2,000 psi, and inspect for kinks or damage before each use. Keep the operator’s station free of clutter, and install a spill containment mat to catch any accidental oil leaks. Finally, conduct a pre‑operation checklist that includes verifying the integrity of the hydraulic reservoir, confirming the correct fluid level, and ensuring the bender’s safety interlocks are engaged. Only trained personnel should operate the machine after completing this safety briefing. Additionally, operator should verify that the hydraulic reservoir is free of debris and that the reservoir cap is tightly secured to prevent leaks. The hydraulic hoses must be inspected for cracks or wear before each shift, and any damaged hose should be replaced immediately. The machine’s safety interlock system should be tested at the start of each day to confirm that it prevents the bender from operating when the safety guard is open. The facility should maintain a log of all maintenance activities, including hose replacements, bearing changes, and any incidents. A dedicated spill kit should be positioned within 10 ft of the machine to quickly contain any accidental oil leaks. Finally, the operator should review the safety briefing before each shift to ensure compliance with all procedures!
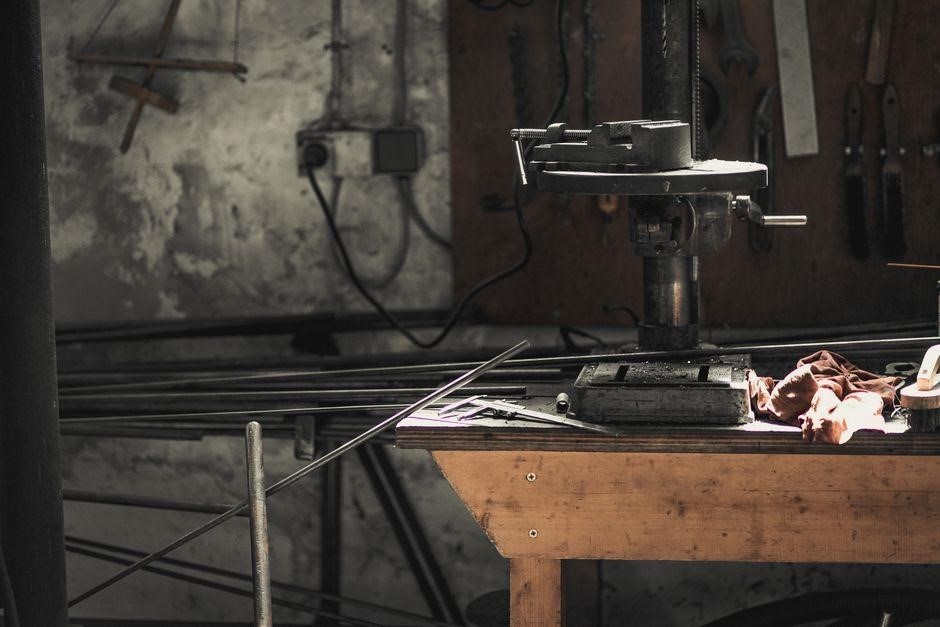
Mounting the Bender on the Pedestal
Before mounting the Hossfeld Universal Bender, ensure the pedestal is level and firmly anchored to the floor. Use a calibrated spirit level to verify horizontal alignment, then secure the pedestal with concrete anchors or steel brackets, depending on the floor type. Once the pedestal is stable, position the bender’s base plate onto the pedestal’s mounting flange. Align the plate’s bolt holes with the pedestal’s threaded studs, and tighten the set screws in a cross‑pattern to distribute clamping force evenly. Next, attach the hydraulic cylinder to the bender’s mounting bracket using the supplied fittings and check for proper seal integrity. Verify that the cylinder’s piston rod is free of obstructions and that the hydraulic fluid line is correctly routed to the pump. After securing the cylinder, install the roller assembly by aligning the roller shaft with the bender’s roller bearing and tightening the locking nuts. Finally, perform a test run without stock to ensure all components move smoothly, and adjust any misalignments before proceeding to actual bending operations. This systematic mounting procedure guarantees structural stability, optimal hydraulic performance, and safe operation for all users.
During installation, always double‑check torque specifications for all mounting bolts, ensuring they meet the manufacturer’s recommendations. Use a calibrated torque wrench to apply the correct force, preventing over‑tightening that could damage threads or under‑tightening that might lead to wobble. Inspect the pedestal’s bearing surface for scratches or debris before placement, and clean it with a solvent to promote a smooth interface. Additionally, verify the hydraulic reservoir is positioned within the recommended clearance to avoid spills during operation.
Operation and Bending Techniques
The hossfeld bender instruction manual guides operators through hydraulic controls, load settings, and precision alignment; It outlines procedures for basic, U‑bends, and irregular shapes, emphasizing safety, pressure limits, and material‑specific schedules. Proper technique ensures consistent, accurate bends every time.
Performing Basic Bends
To perform a basic bend with the Hossfeld Universal Bender, begin by verifying the hydraulic system is fully charged and the safety interlocks are engaged. Position the workpiece on the 9B flat‑surface roller, ensuring the bar or angle iron lies flush against the roller’s face. Align the workpiece’s centerline with the pivot point of the hydraulic cylinder. Use the built‑in angle gauge to set the desired bend angle; for a 90° bend, rotate the gauge until the indicator reads 90°, then lock the gauge in place. Engage the hydraulic master cylinder, applying pressure gradually while monitoring the pressure gauge; the system typically requires 15–20 psi for mild steel and 25–30 psi for stainless steel. Once the pressure stabilizes, release the safety lock to allow the cylinder to move. The hydraulic piston will push the workpiece against the roller, forming the bend. After the cylinder reaches the end of its travel, the system will automatically lock the piston in the bent position. Carefully remove the workpiece, inspect the bend for uniformity, and check the angle with a protractor. If the bend is not within tolerance, adjust the gauge and repeat the process, ensuring the workpiece remains centered on the roller throughout. Finally, release the hydraulic pressure, disengage the safety lock, and store the bender in a clean, dry environment to prevent corrosion.
Before starting, inspect the roller for wear and replace if necessary; a worn roller can cause uneven bends or surface damage. The 11B square blocks and pins should be positioned according to the workpiece’s cross‑section; for round stock, use the 11B block, and for flat stock, use the 9B roller. Ensure pins are fully seated in the block to maintain alignment. After each bend, clean the roller and block surfaces with a solvent to remove metal shavings, preventing future binding. The manual also recommends performing a quick test bend on a scrap piece to confirm the system’s readiness; this test should replicate the intended bend angle and material thickness. If the test bend shows any deviation, recalibrate the hydraulic pressure or adjust the angle gauge. The Hossfeld Universal Bender’s design allows for incremental angle adjustments, so small changes can be made without disassembling the machine. Always wear appropriate PPE, including gloves and eye protection during operation. By following these steps, operators can achieve precise, clean bends that meet engineering specifications and maintain the longevity of both the workpiece and the bender itself.
Bending Angles and U-Bends
The Hossfeld Universal Bender’s angle gauge and hydraulic system enable precise control over bending angles ranging from 10° to 180°. To perform a U‑bend, first secure the workpiece on the 9B flat‑surface roller and align the pivot point with the bar’s centerline. Set the target angle on the gauge, lock the setting, and engage the hydraulic cylinder. The piston pushes the workpiece against the roller until the desired angle is achieved, then the system locks the bend automatically. For angles above 90°, the manual advises increasing hydraulic pressure by 5 psi for every 10° beyond 90° to preserve material integrity and prevent cracking. After the bend, use a caliper to verify the U‑profile’s radius and ensure uniform thickness. The manual recommends a quick test: quickly bend a scrap piece at the intended angle, measure the radius, and compare to the manufacturer’s specifications. If the radius is off, adjust the pressure or reposition the roller to correct the bend. Proper lubrication of the roller and pins is critical, especially for tight U‑bends, to reduce friction and extend component life. The hydraulic system is calibrated for a variety of materials, including mild steel, stainless steel, and aluminum, by selecting the appropriate pressure range. Operators should also check the angle gauge for calibration before each session to maintain accuracy. By following these procedures, users can achieve consistent, repeatable bends that meet engineering tolerances, reduce waste, and prolong the machine’s operational lifespan.
Irregular Shapes and Offset Bending
Operating the Hossfeld Universal Bender for irregular shapes and offset bending requires a clear understanding of the machine’s adjustable die system and the precise control of hydraulic pressure. Begin by selecting the appropriate die plate that matches the desired curvature radius; the manual specifies a range of 1.5 to 6 inches for typical steel grades. Once the die is mounted, adjust the offset lever to the required offset distance, ensuring the lever is fully engaged to lock the die in place. Next, position the workpiece on the roller bed, aligning the centerline with the die’s axis. The manual recommends using a 0.25‑inch clearance on the opposite side to prevent binding during the bend. Before initiating the hydraulic cycle, verify that the pressure gauge reads within the recommended 150–200 psi range for mild steel; for stainless or alloy steels, lower the pressure to 120–150 psi to avoid cracking. Engage the hydraulic pump slowly, allowing the system to build pressure gradually. The instruction manual advises a 3‑second dwell time after reaching target pressure before releasing the brake. This dwell period ensures the metal fully conforms to the die shape. During the release, the brake should disengage smoothly; any resistance may indicate a misaligned die or insufficient clearance. After completing the bend, inspect the workpiece for uniformity. The manual provides a tolerance chart: for a 30‑degree offset bend, the deviation should not exceed 0.010 inches; If the bend is too shallow, increase the pressure by 10 psi increments and repeat the cycle. For deeper bends, adjust the offset lever by 0.125 inches increments and re‑calibrate the die. The Hossfeld manual also highlights the importance of using a lubricant on the die surface to reduce friction when working with alloys.! Finally, record the pressure, die setting, and offset distance in the logbook for future reference, as consistency is key to achieving repeatable results across multiple pieces.
Cold-Bend Schedule for Various Materials
The hossfeld bender instruction manual provides a detailed cold‑bend schedule that aligns with industry standards for common metals. The table below lists recommended bend radii, maximum bend angles, and material thickness limits for each alloy. These guidelines help operators avoid cracking, springback, and excessive wear on the hydraulic system.
- Carbon Steel (A36): Thickness 0.020–0.060 in. – Bend radius 1.5× thickness, max angle 90°, 0.060‑in. stock may be bent to 120° with a 2× thickness radius.
- Stainless Steel (304/316): Thickness 0.015–0.050 in. – Bend radius 2× thickness, max angle 90°, 0.050‑in. stock to 120° requires 3× thickness radius.
- Aluminum (6061): Thickness 0.010–0.040 in. – Bend radius 2.5× thickness, max angle 90°, 0.040‑in. stock to 120° needs 4× thickness radius.
- Cast Iron: Thickness 0.020–0.060 in. – Bend radius 3× thickness, max angle 60°, 0.060‑in. stock to 90° requires 4× thickness radius.
- Nickel‑Alloy (Inconel 718): Thickness 0.008–0.030 in. – Bend radius 3× thickness, max angle 90°, 0.030‑in. stock to 120° needs 5× thickness radius.
For each material, the manual recommends a pre‑bend inspection step: verify the surface for defects, clean the stock, and apply a light lubricant to reduce friction. After the bend, allow the part to cool to ambient temperature before measuring the final angle. The schedule also includes a springback correction factor (typically 2–5% of the target angle) that should be applied when programming the hydraulic cycle time. Operators should record each bend in a logbook, noting material, thickness, radius, angle, and any deviations from the schedule. This practice ensures traceability and facilitates future maintenance of the Hossfeld Universal Bender.
The manual also stresses the importance of maintaining the hydraulic fluid level within the specified range (5–7 gallons) and checking for leaks before each session. A proper purge cycle eliminates air pockets that can compromise the bend quality. Calibration of the pressure gauge to ±5 psi ensures consistent force application across all materials. Operators should perform a test bend on a scrap piece before committing to production runs, verifying that the achieved angle matches the target within the acceptable tolerance band of ±0.5°.
When bending thicker sections, the manual advises using a double‑roller setup to distribute load evenly and reduce the risk of pin bending. For irregular shapes, a custom jig can be fabricated from steel plates and bolted to the base plate; the jig should be aligned with the desired bend line and secured with locking bolts. The manual also includes a troubleshooting matrix that lists common issues such as excessive springback, uneven bends, or hydraulic pressure drops, along with corrective actions.
Finally, the hossfeld bender instruction manual recommends a quarterly inspection of the hydraulic cylinder, seals, and piston rod for wear. Replace worn components immediately to avoid catastrophic failure. Keeping a detailed maintenance log not only extends the life of the machine but also provides valuable data for future upgrades or modifications.